
Capabilities
5-axis CNC machining, EDM and grinding under one roof
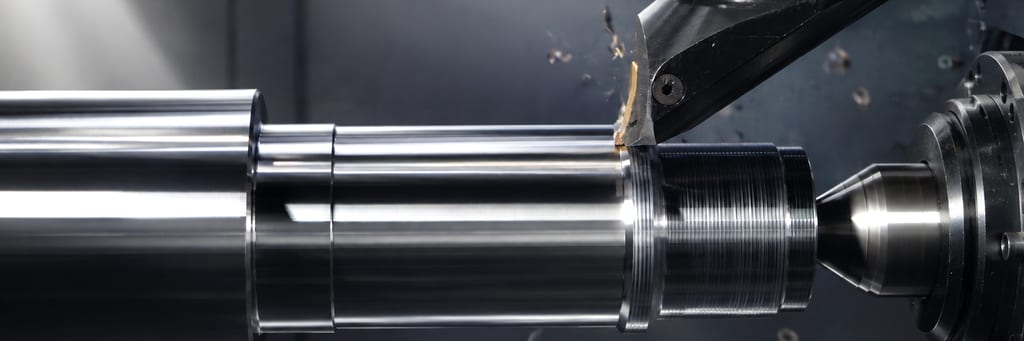
From design and programming, through 5-axis CNC machining, EDM and grinding, to assembly and trial runs — without relying on subcontractors.
Why in our own shop
One shop, one party responsible
When a tool is made across several subcontractors, every mistake becomes somebody else's. Deadlines slip while you wait for a slot on another firm's machine, and when something is wrong, nobody is sure at which stage it happened.
That is why we keep the whole chain in house. If a trial shows a cavity needs correcting, the correction goes onto our own machine the same day rather than into somebody else's queue.
These machines produce our injection moulds, stamping dies and PET blow moulding machines; how we check dimensions is described under quality control.
- Design and programming
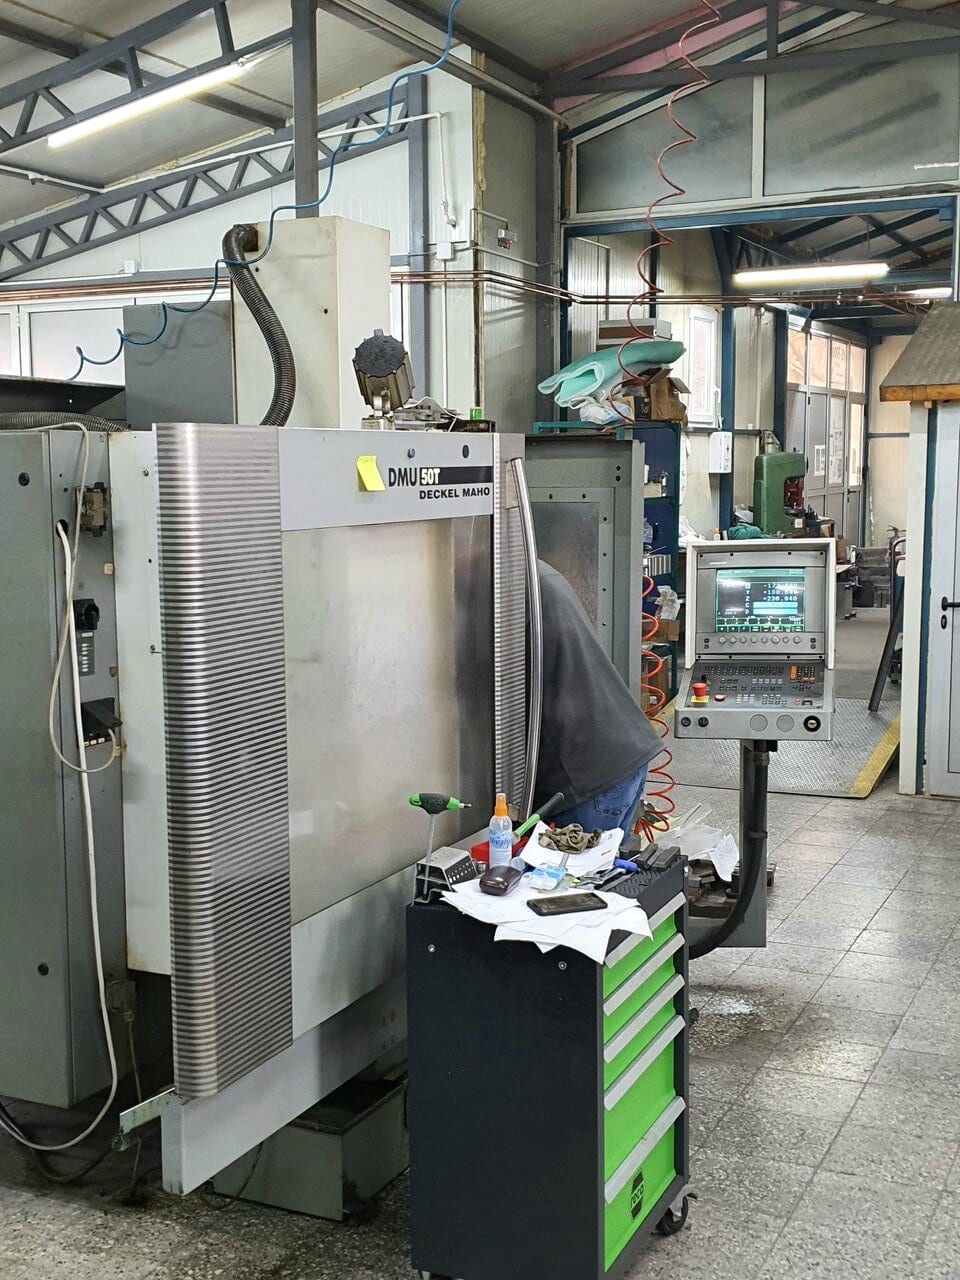
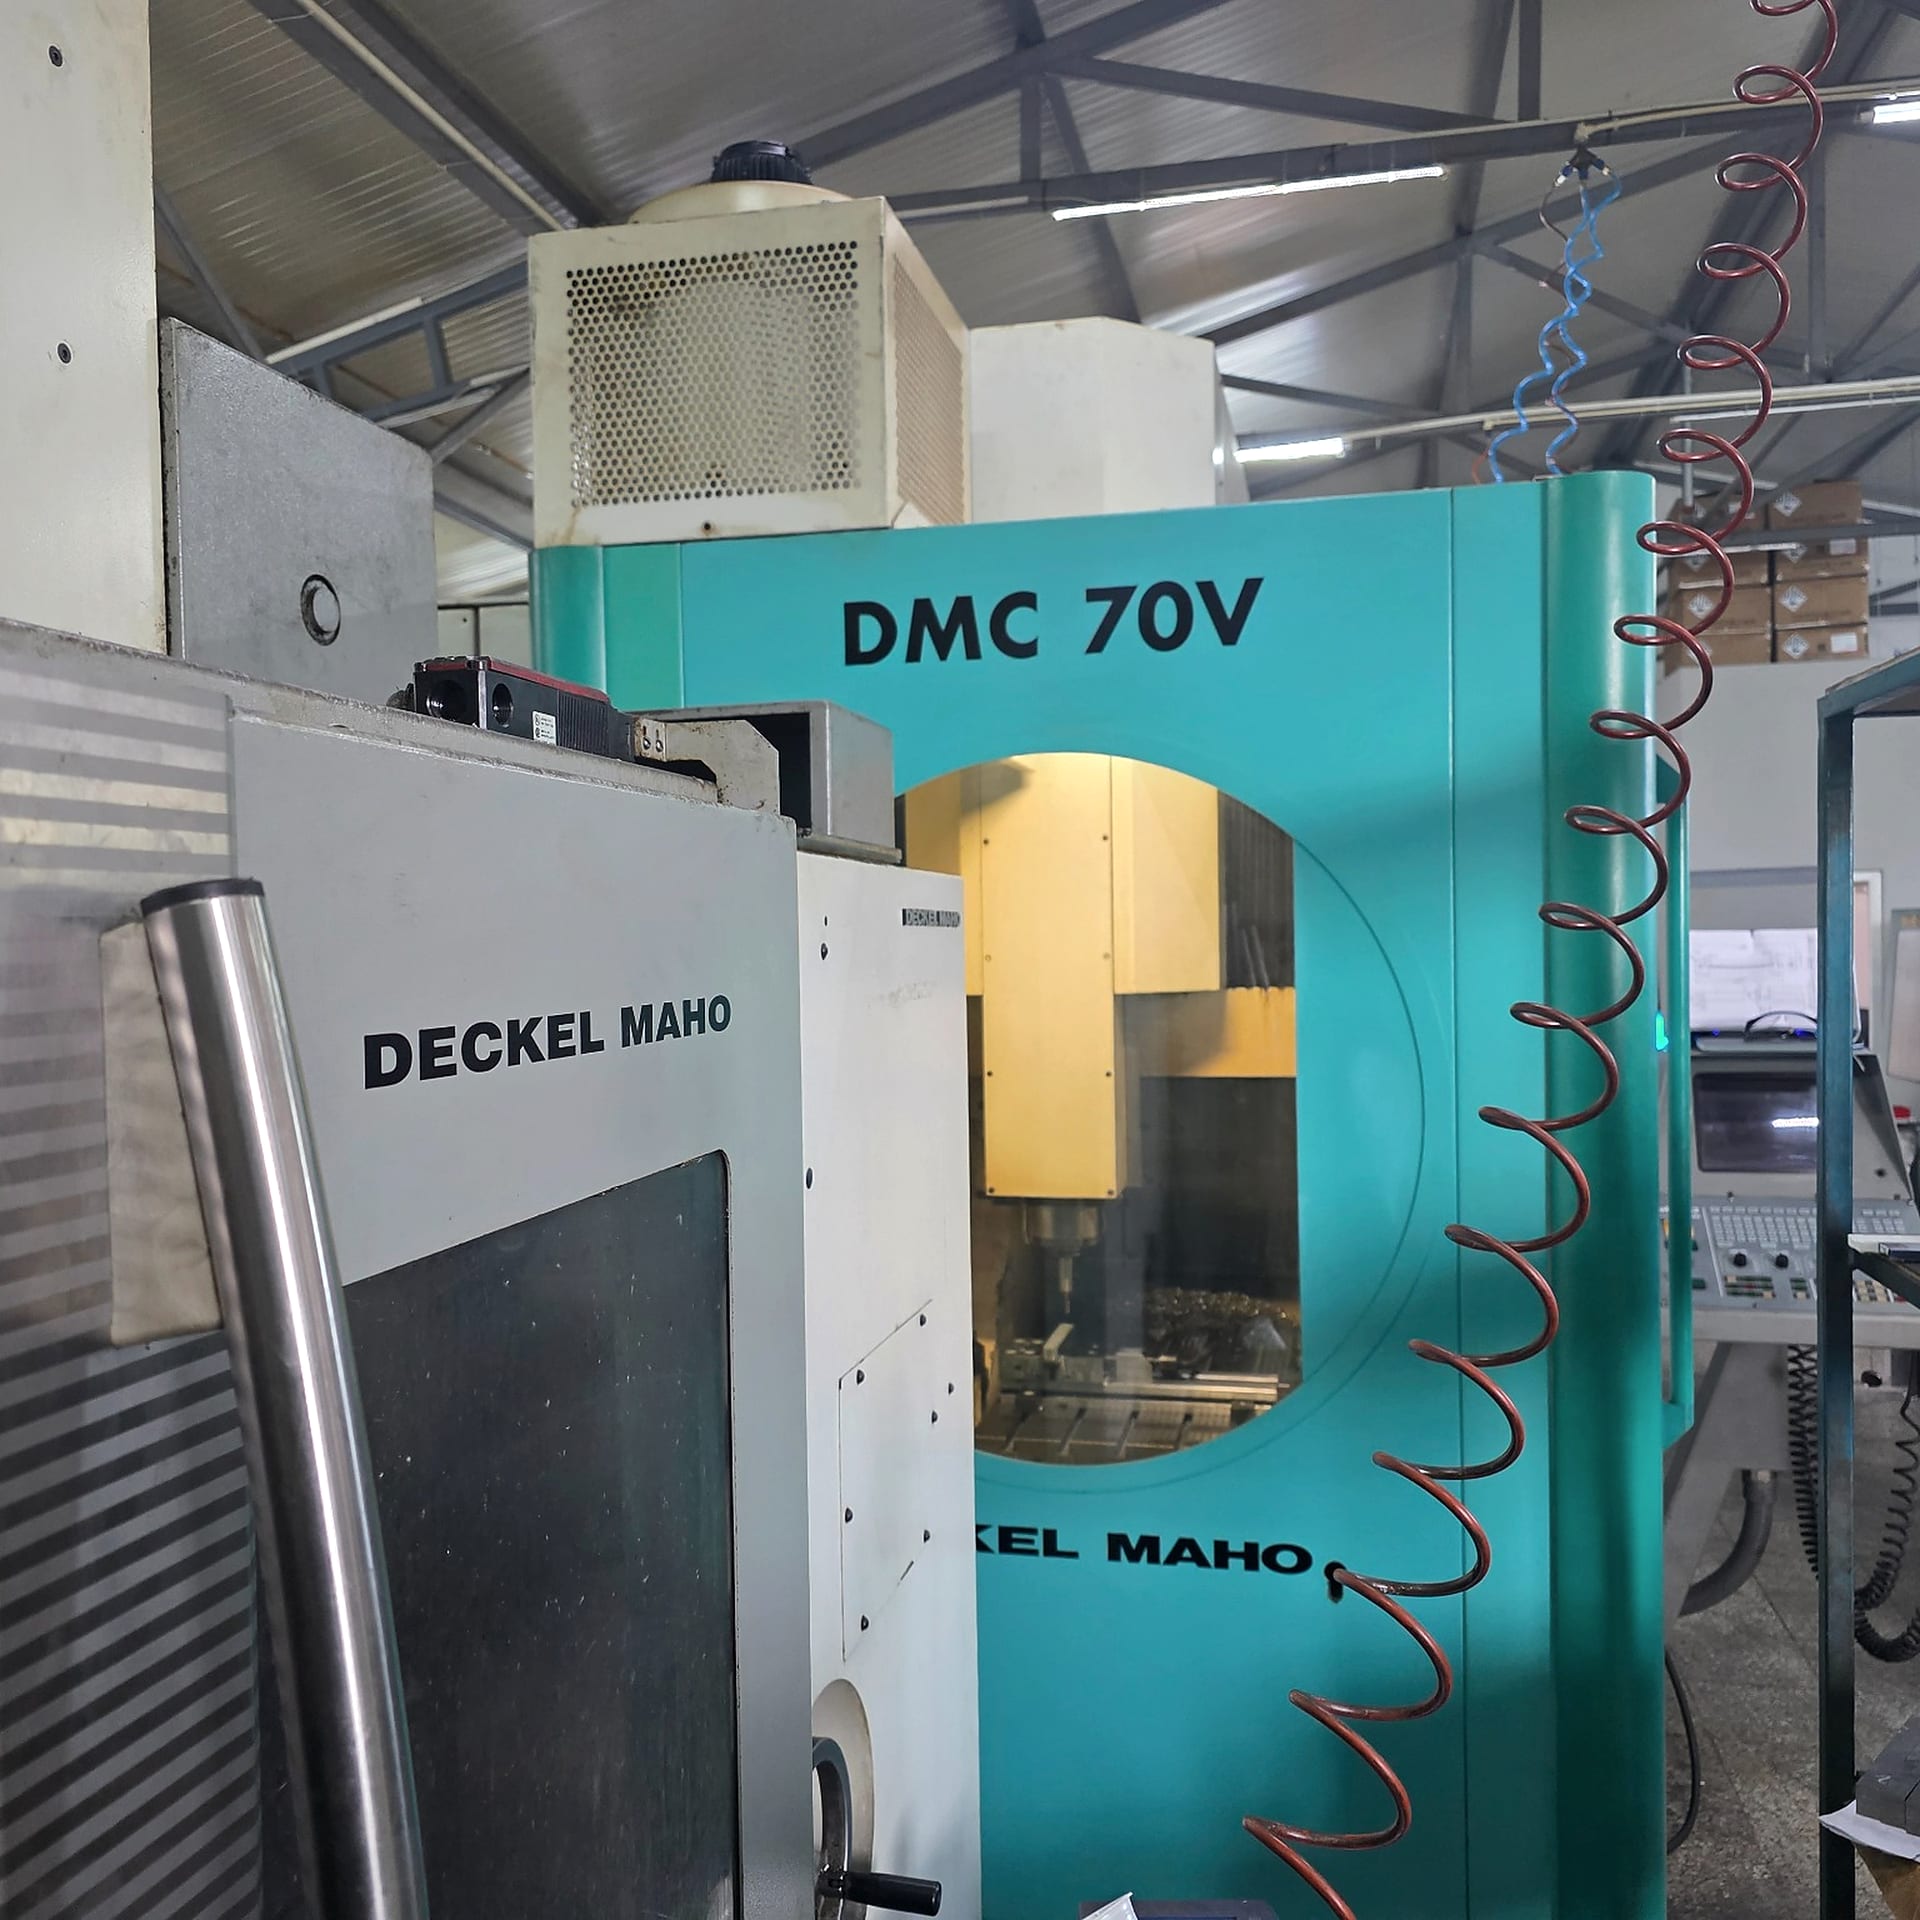
- Roughing and finish milling, up to five axes
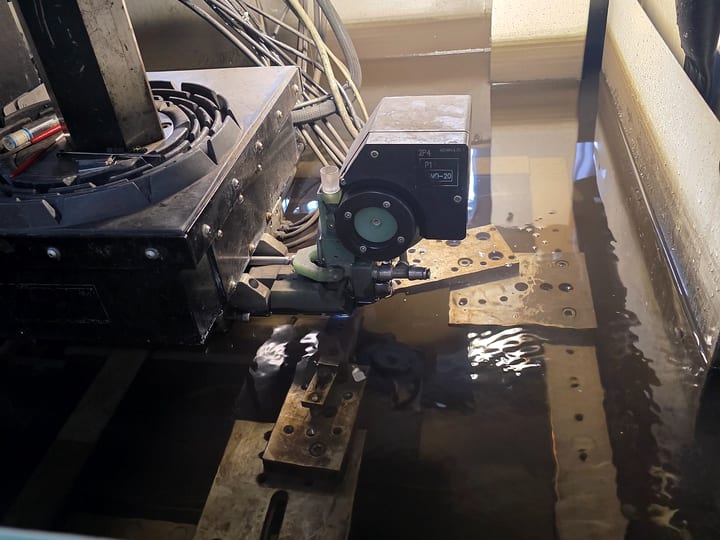
- Die-sinking EDM for cavities, ribs and sharp internal corners
- Wire EDM for hardened components
- Surface grinding of mating faces
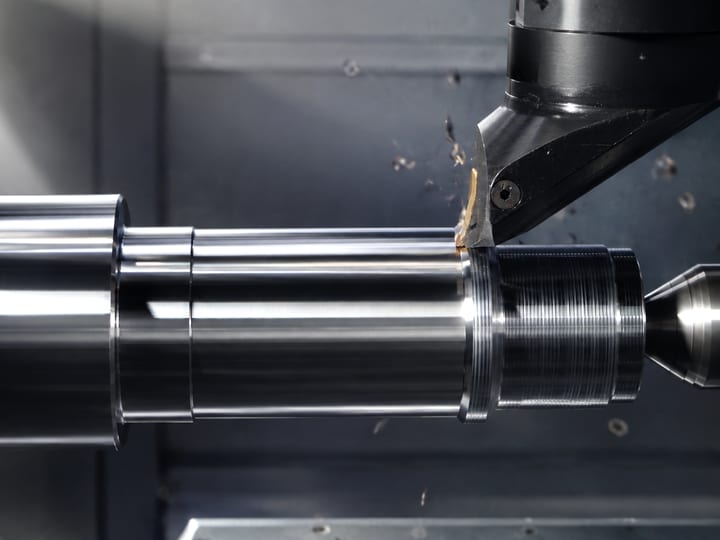
- Turning on manual and programmable lathes
- Assembly, trial runs and dimensional inspection before despatch
Machine park
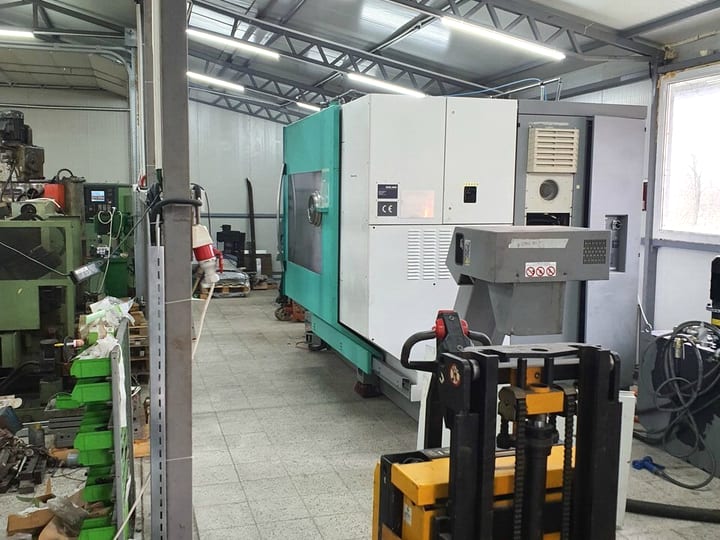
Machine park: mills, EDM, lathes and a surface grinder
The machines we run, from milling to EDM, grinding and turning — all in the same shop.
| Machine | Note |
|---|---|
|
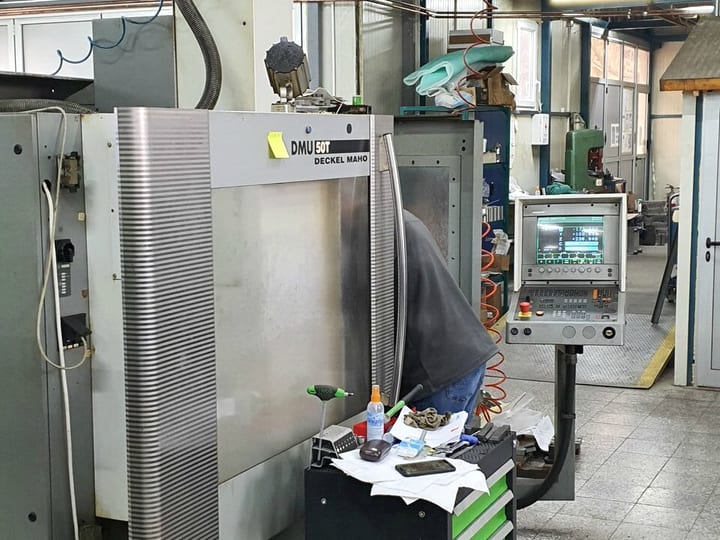
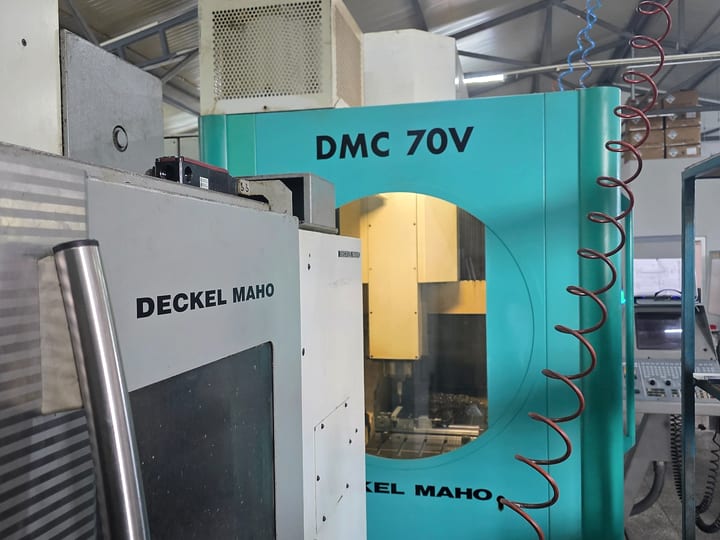
Roughing and finishing of plates and cavities, fourth-axis indexing and simultaneous five-axis machining of complex forms, up to 5 axes. Among them a DECKEL MAHO DMC 70 V and a DMU 80 P. |
| Large-format CNC milling machine | One of the 11 mills · Axis travels X 2,500 × Y 1,000 × Z 1,000 mm (98.4 × 39.4 × 39.4 in) |
|
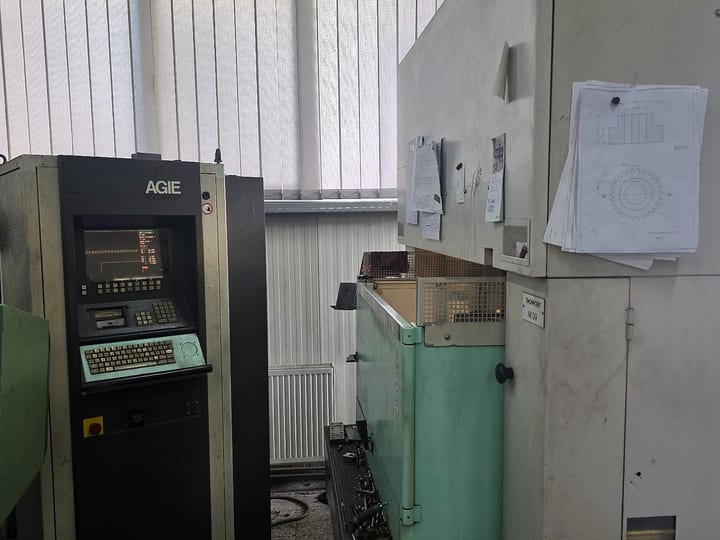
Deckel DE 25 · die-sinking — cavities, ribs and sharp internal corners |
| 1 × CNC wire EDM | Hardened stamping die components |
|
Finishing of mating faces |
| 1 × Universal lathe | Turned parts and modifications |
| 1 × Programmable lathe | Series production of turned parts |
| 1 × Tool sharpener | Cutting-tool maintenance |
| 1 × Circular metal cutting saw | Stock preparation and cut-to-length |
Photographs
Machines on the shop floor
-
-
-
-
-
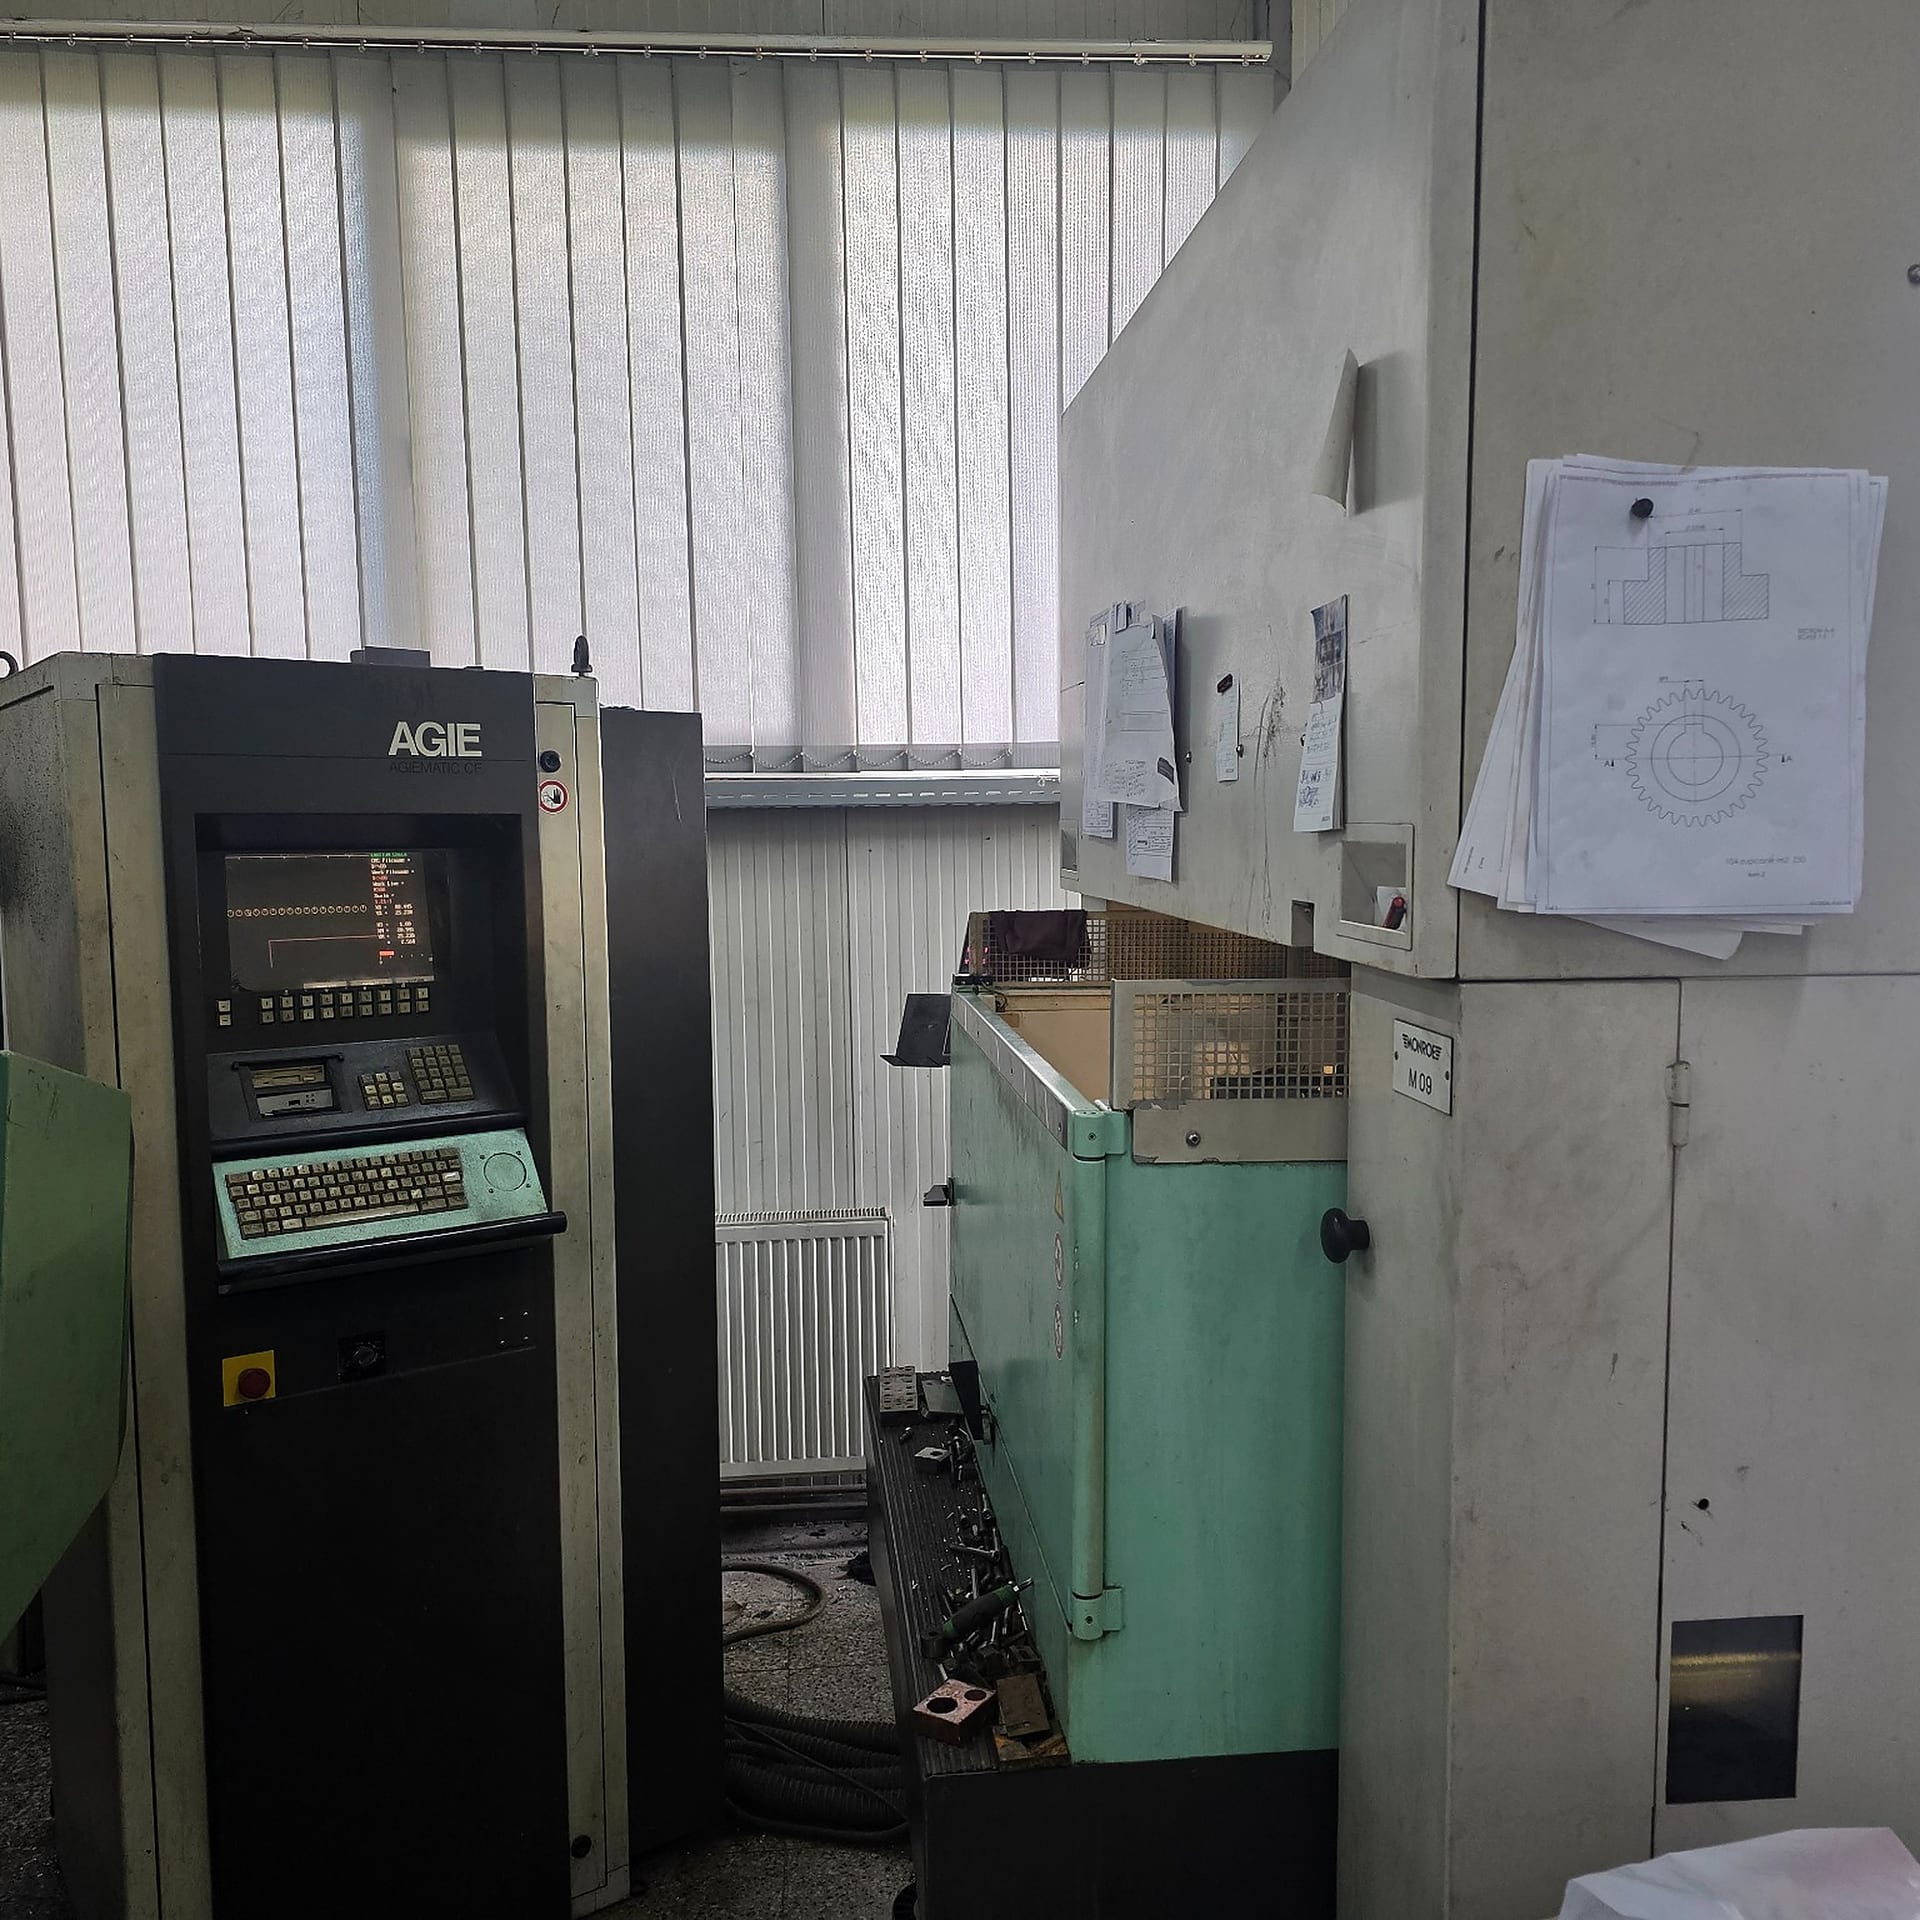
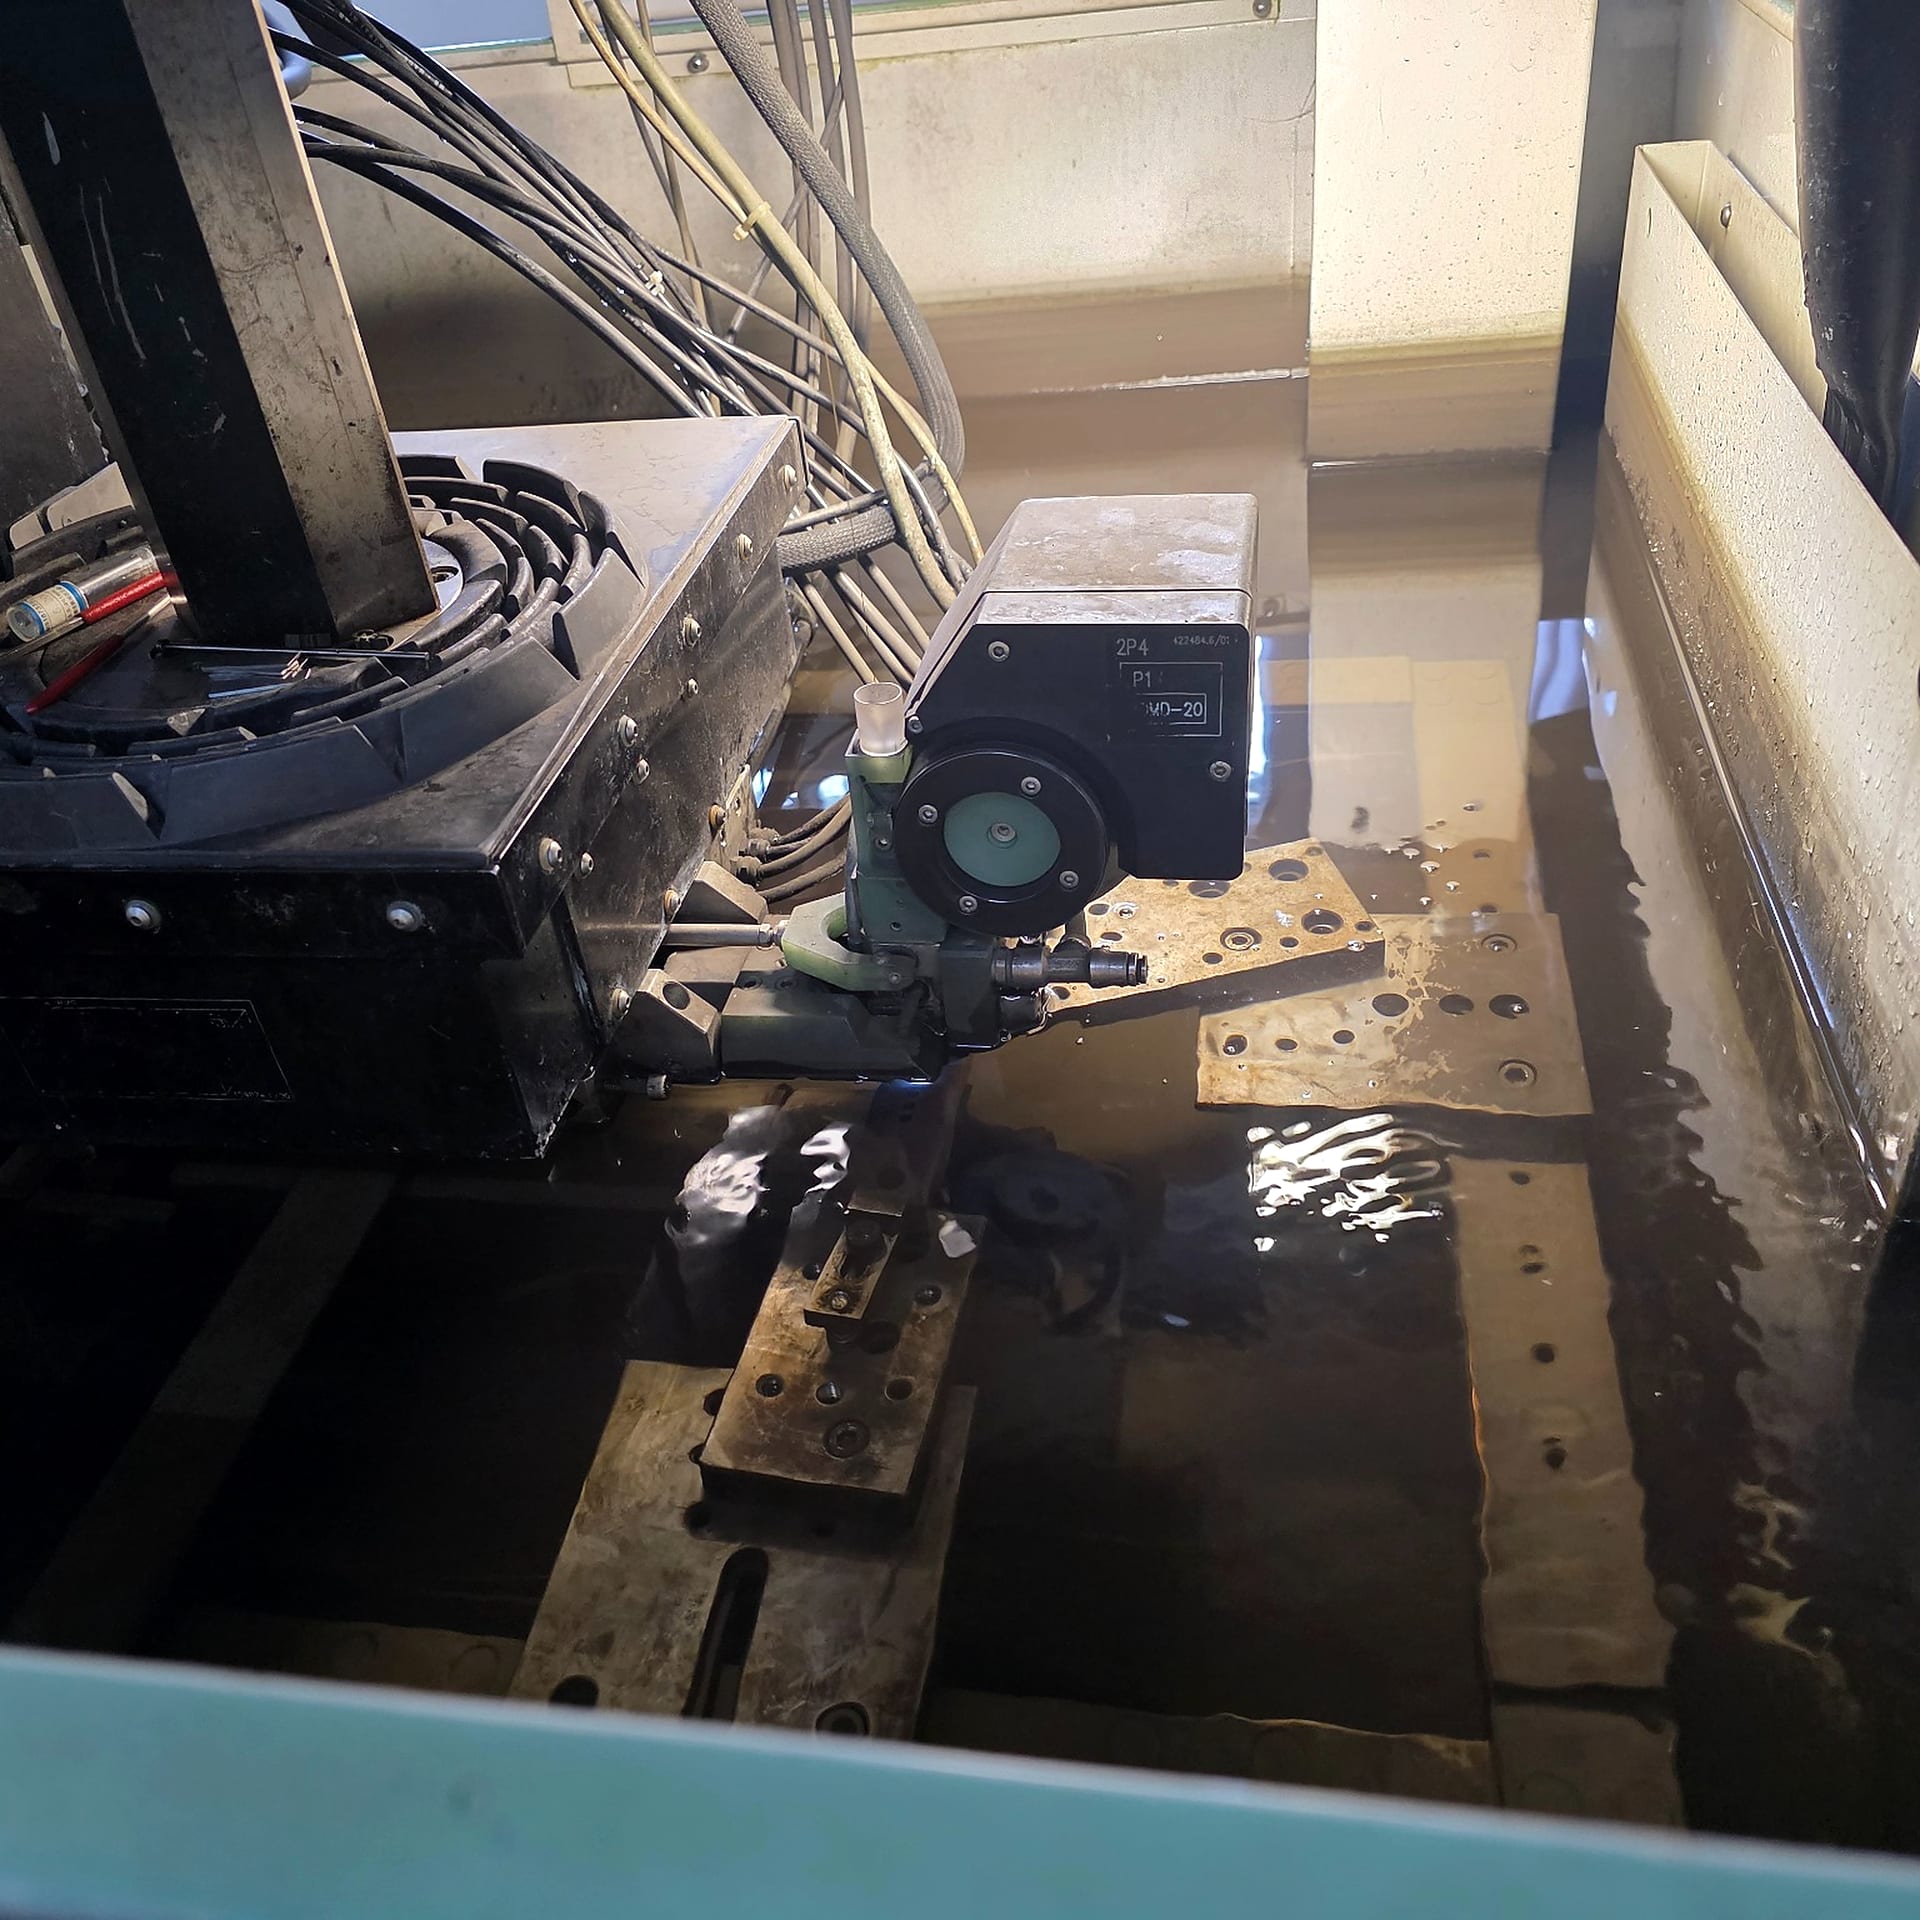
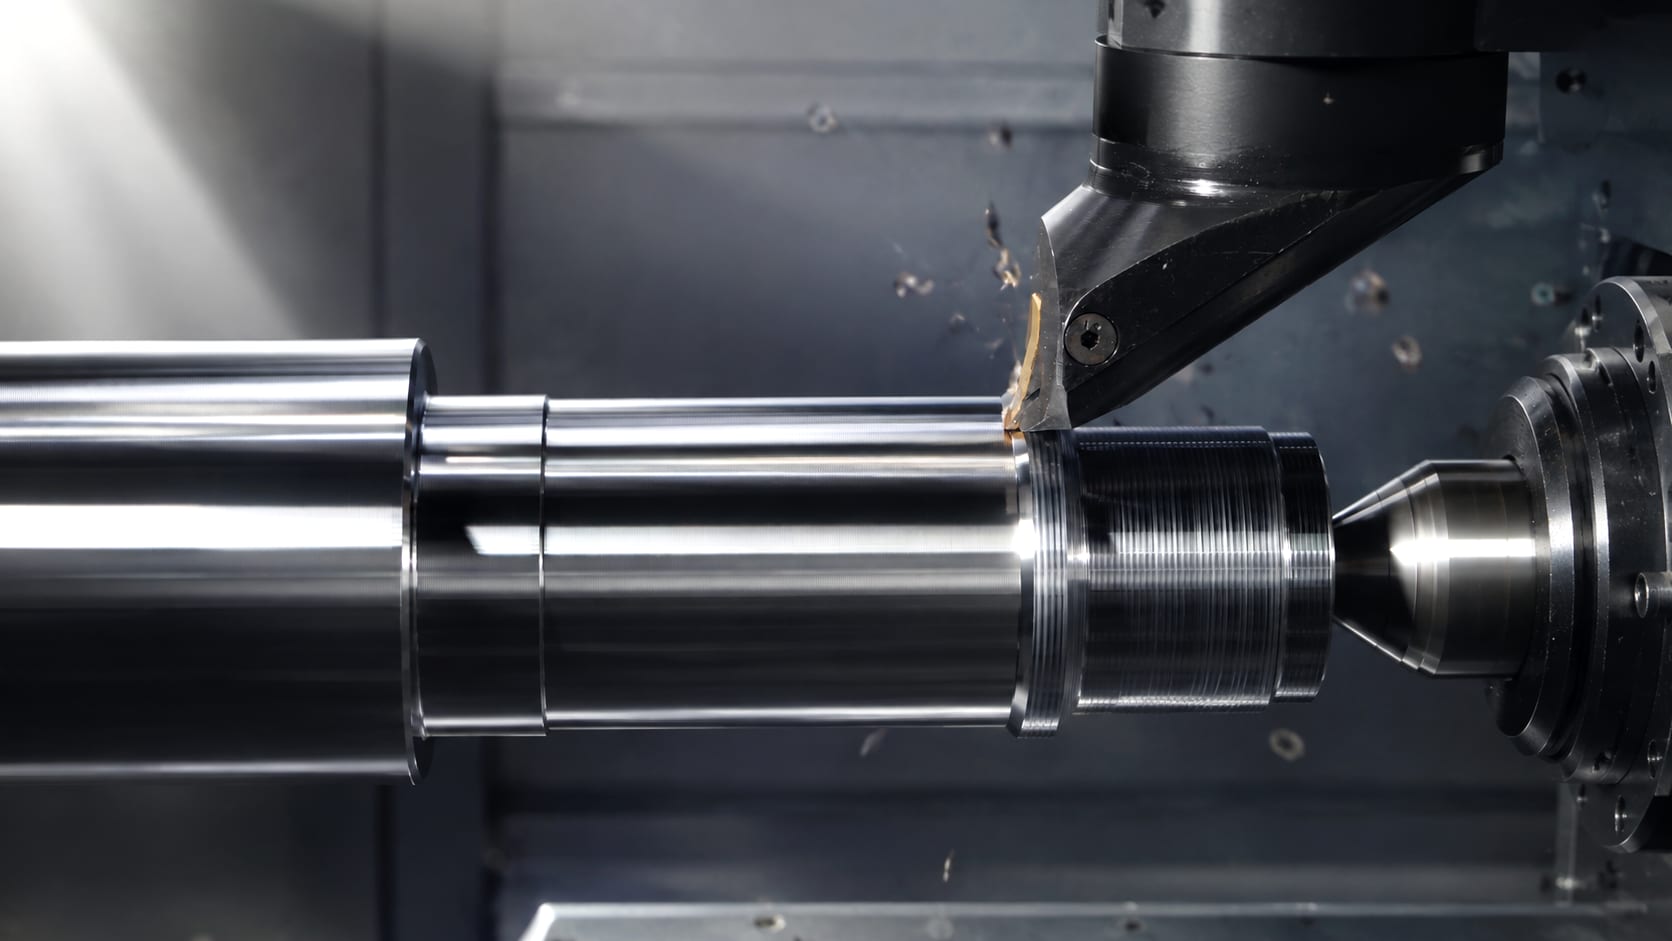
Photographs of the wire EDM and the surface grinder will be added once they have been taken.
Materials
What we machine
The toolroom works mainly in tool steels, both annealed and hardened. Hardened components are finished by EDM and grinding, because that is the only way to hold size after heat treatment.
Alongside steel we regularly machine aluminium and non-ferrous metals, most often for machine parts, fixtures and ancillary tooling.
Process
What every tool goes through
-
01
Design
Model and drawing, parting line, guiding, cooling. This is where problems get solved that would otherwise only surface at the trial.
-
02
Roughing
Milling of plates and blanks on CNC machines, leaving stock for finishing and for heat treatment.
-
03
EDM
Cavities and sharp internal corners by die-sinking EDM; hardened components by wire EDM, after hardening rather than before.
-
04
Grinding
Surface grinding of the mating faces, which decide whether the tool seals and whether the halves align.
-
05
Assembly
Assembly, checking of travel and sealing, and preparation for the trial.
-
06
Trial
Trial run and dimensional inspection. No tool goes to the customer until it produces a sound part.
Questions
Common questions about our machine park
What is the largest part you can machine?
Our largest CNC milling machine has axis travels of X 2,500 × Y 1,000 × Z 1,000 mm (98.4 × 39.4 × 39.4 in). The part size you can actually machine also depends on fixturing and tooling, so send us the drawing and we will tell you straight away whether we can take it on.
How many CNC milling machines do you have?
We have 11 CNC milling machines — three-, four- and five-axis — one of them a large-format machine. Alongside them the shop runs a sinker EDM, a wire EDM, a surface grinder, and universal and programmable lathes.
How many axes do you machine in?
Up to five, including simultaneous five-axis machining of complex forms.
Do you machine hardened parts?
Yes. Hardened parts are finished by EDM and grinding, because that is the only way to hold a dimension after heat treatment.
Next step
Tell us what you need
Send a drawing, a model, or simply a description of the job. We will come back with the scope, the price and the schedule.